A comprehensive technical brief designed for brand directors, commercial buyers, and supply chain orchestrators navigating high-yield OEM/ODM production matrices.
The contemporary hobo silhouette has transcended unstructured bohemian aesthetics. Current commercial metrics necessitate precise crescent tailoring, dynamic load distribution across seamless shoulder straps, and modular interior compartmentalization designed for modern digital devices.
By implementing 3D CAD pattern grading and automated hydraulic hide-nesting, leading Chinese exporters minimize cut-loss variance below 2.4% while preserving authentic drape dynamics across top-grain cowhide substrates.
Global regulatory landscapes require comprehensive traceability down to raw hide origins. Exporting factories partner exclusively with Leather Working Group (LWG) certified tanneries, ensuring zero hexavalent chromium (Cr VI) generation and rigorous wastewater management protocols.
Adherence to EU REACH standards and US Proposition 65 ensures all electroplated hardware finishes (zinc alloy, solid brass, and anti-corrosion magnetic closures) remain free from nickel migration, lead, and phthalate plasticizers.
Addressing inventory volatility in post-pandemic retail, contemporary Chinese manufacturing clusters maintain lean production lines capable of supporting pilot runs starting at 200 units per colorway, transitioning smoothly to high-capacity yields exceeding 60,000 units monthly.
Digital technical packs (tech packs) are typically translated into fully operational master physical samples within 5 to 7 business days, enabling brands to execute rapid speed-to-market testing.
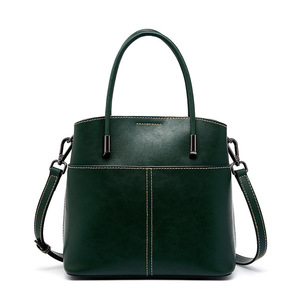
Explore high-volume OEM/ODM silhouettes spanning classic crescent forms, multi-piece sets, high-tensile briefcases, and precision small leather goods.
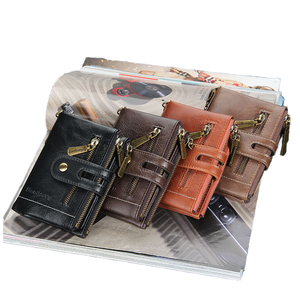
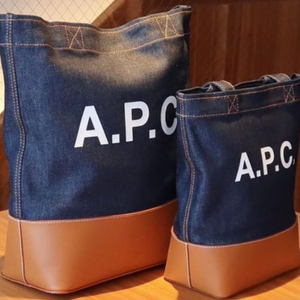
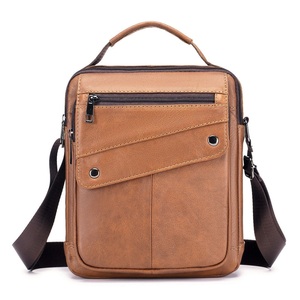
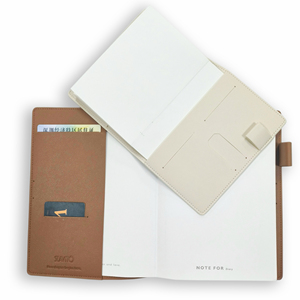
Quantitative projections on raw material fluctuations, sustainable finishing technologies, and automated manufacturing lines impacting direct landed costs.
Procurement teams are aggressively shifting toward metal-free (wet-white) and aldehyde-free vegetable tanning to satisfy incoming European Corporate Sustainability Due Diligence Directives (CSDDD). Vegetable-tanned Italian-grade pull-up hides are undergoing bio-finish treatments using beeswax and plant oils to maintain slouch while resisting hydro-penetration.
Expect +38% demand growth for fully traceable, chrome-free top-grain cowhide substrates within premium hobo categories across mid-to-high tier retail portfolios.
Traditional hand-skiving and mechanical clicker presses are transitioning to CNC multi-axis oscillating knife cutting tables. Digital camera vision systems scan individual hides, detect natural scar defects, grain inconsistencies, and insect bites in real time, and adjust nesting vectors automatically.
This automated skiving and cutting infrastructure increases yield efficiency by up to 14%, directly neutralizing upward wage pressure and stabilizing wholesale FOB quotations.
Forward-thinking exporters are embedding ultra-thin NFC and RFID chips within the interlining of leather shoulder straps and gusset linings. These micro-transponders hold encrypted supply chain provenance data, validating tannery audit certificates, carbon footprint calculations, and authenticity certifications directly at retail checkout.
Implementing DPP infrastructure reduces customs clearance friction across EU/NA transit ports by over 30% through automated customs compliance validation.
| Substrate Material Class | Tensile Strength (N/mm²) | Moisture Retention (%) | LWG Compliance Index | Optimal Commercial Application |
|---|---|---|---|---|
| Full-Grain Calfskin (0.9–1.1mm) | 18.5 – 22.0 | 12% – 14% | Gold Rated / Traceable | Luxury Slouch Hobo Bags, Minimalist Totes |
| First-Layer Cowhide (1.2–1.4mm) | 22.5 – 26.0 | 10% – 13% | Silver/Gold Certified | Structured Crescent Hobos, Heavy Shoulder Bags |
| Split Leather with PU Lamination | 14.0 – 17.5 | 6% – 8% | Chemical REACH Compliant | Fast-Fashion Commercial Sets, High-Volume Retail |
| Waterproof Technical PU Leather | 12.0 – 15.0 | < 2% | Non-Animal / Oeko-Tex Standard | Cosmetic Organizers, Weatherproof Multi-Piece Sets |
From internal edge-painting chemistry to seam reinforcement under structural fatigue testing.
The defining failure point of lower-tier hobo shoulder bags is cracked or peeling edge paint along the high-flex strap arc. Our industrial protocol enforces a 5-step hand-rubbed edge finish: primer bonding, double Italian polyurethane resin layering, thermal smoothing at 140°C, and final matte sealing.
This guarantees flexural integrity across extreme temperature gradients (-20°C to +45°C) without cracking or stickiness under high humidity conditions.
Hobo bags rely on fluid drape dynamics, yet commercial buyers demand the capacity to support up to 8kg of everyday carry items. To achieve this without distorting the silhouette, specialized non-stretch microfiber interlinings and bonded nylon thread (Tex-70 to Tex-90) are integrated internally along the main handle roots.
Seams undergo strict tension load testing, surviving 5,000 cycles on pneumatic jolt testing rigs without seam slippage or fiber detachment.
Marine-grade electroplating methods prevent tarnishing, oxidation, and scratches on buckles, swivel snap hooks, and custom brand nameplates. Utilizing multi-layer copper-nickel-chrome or PVD vacuum coating, every metallic component withstands a minimum of 48-hour neutral salt spray (NSS) testing.
Smooth zipper glide operations are preserved using custom heavy-duty metal teeth with deburred edges, paired with smooth nylon slide tapes.
Direct technical and commercial responses addressing common challenges encountered by sourcing directors and international buyers.
Prototyping and sample refinement require 5 to 7 business days. Upon final counter-sample approval, material lab dip confirmation, and receipt of deposit, bulk mass manufacturing cycles run between 30 and 45 calendar days, contingent on bespoke hardware tooling requirements and order quantities.
We deploy spectrophotometer spectrophotometric color matching under standard D65 illuminant light cabinets. Delta-E variance is strictly maintained below 0.8 across distinct hide lots. Master swatches from every approved tannery drum lot are archived for up to 24 months to ensure exact seasonal re-order matching.
Production follows the ISO 2859-1 (AQL 1.5 / 2.5 Major/Minor) standard. Our inline Quality Assurance (QA) team monitors hide preparation, adhesive solvent dissipation, seam stitch pitch (consistently calibrated to 7–8 stitches per inch), and handle tensile durability before final packaging.
Yes. We operate internal mold tooling facilities for die-cast zinc alloy, CNC-machined brass, debossed foil badges, and custom laser-engraved zipper pulls. Custom hardware molds typically require 10 to 12 days for sample strike-offs and testing prior to bulk electroplating.
Every export consignment includes full material declarations: LWG tannery certificates, REACH SVHC compliance dossiers, fumigation documentation for wooden packaging materials, and optional carbon calculation manifests to assist tier-1 brand reporting obligations.
Connect directly with our engineering department to evaluate tech packs, request material swatches, or schedule a virtual audit of our assembly lines.
Contact Us