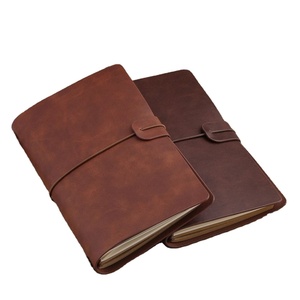
Custom Logo A5 Leather Refillable Travel Journal Notebook
- TannageFull Veg-Tan Cowhide
- ApplicationCorporate & Hospitality
- CustomizationDebossed / Refillable
Explore production-grade full-grain vegetable-tanned articles, technical microfiber upholstery, and artisanal leather accessories formulated specifically for moisture-heavy tropical environments and high-traffic regional commercial use.
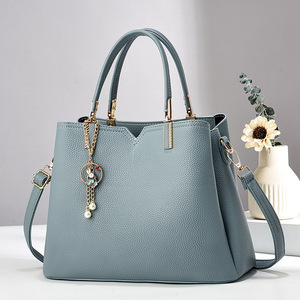
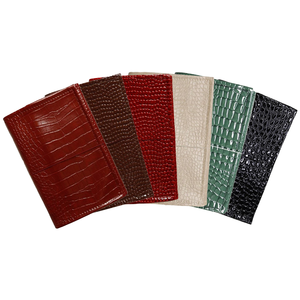
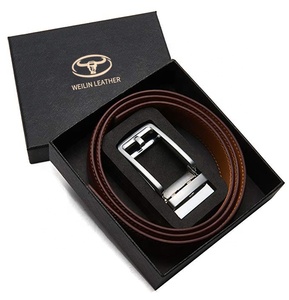
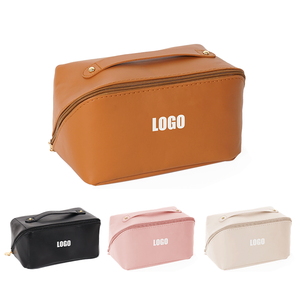
Fully scaled production facility executing private label handbags, accessories, and upholstery hides.
Second-generation, Government of India recognized export house operating ethically under SMETA 4-Pillar audits.
Organic mimosa and quebracho tannin extracts completely free of hexavalent chromium and restricted arylamines.
Panama sits as the premier logistics junction of the Western Hemisphere, anchored by the Colon Free Trade Zone (Zona Libre de Colón) and the Pacific-Atlantic interoceanic transit corridors. However, local climatic conditions—characterized by persistent relative humidity exceeding 85%, high ambient temperatures, and maritime saline exposure—present severe degradation hazards for uncalibrated leather goods.
At our Kolkata production complex, raw hides undergo continuous drum-tanning utilizing controlled concentrations of mimosa, chestnut, and quebracho extracts. This slow vegetable tannage creates dense fiber cross-linking throughout the reticular dermis, preventing grain loose-break while inhibiting mold proliferation without deploying restricted biocides forbidden under European CE and REACH safety guidelines.
The primary point of failure for leather collections deployed in Panama City, Bocas del Toro, and the San Blas maritime sector is hardware oxidization and edge peel. Marine salt mist induces rapid galvanic corrosion on conventional zinc electroplated fasteners, bleeding green copper salts onto raw leather.
To eliminate field returns for high-end Panamanian retailers and hospitality developers, our manufacturing protocols require stainless steel 316 or solid brass substrates treated with Physical Vapor Deposition (PVD) titanium coatings. Furthermore, all edges receive three-stage multi-coat edge polyurethane elastomer finishing, oven-cured to resist thermal softening up to 45°C.
Whether supplying architectural leather panels for luxury resorts in Costa del Este or delivering private label retail collections for international travelers at Tocumen International Airport (PTY), our production maintains zero-defect integrity under the most demanding tropical exposure tests.
Our vegetable-tanned hides and precision OEM assemblies are engineered to support key economic sectors operating across the Republic of Panama and Central American re-export channels.
From heritage boutique hotels in Casco Viejo to high-end rainforest bungalows in Gamboa, hospitality interior designers specify our full-grain veg-tan leathers for bespoke headboards, desk blotters, architectural menu covers, and room folios that age into a warm, natural golden-amber patina without chemical off-gassing.
B2B distributors based in the Zona Libre de Colón rely on our scalable 60,000-unit monthly throughput to source CE-certified small leather goods, executive briefcases, and automatic ratchet belts for onward duty-free distribution across Colombia, Costa Rica, Ecuador, and the wider Caribbean basin with full certificate of origin support.
Panama's massive Pacific and Caribbean marina networks demand specialized seating upholstery. Our technical microfiber and treated veg-tanned bridge leathers pass rigorous Martindale abrasion tests (100,000+ rubs), offering salt-spray, UV-fading, and microbial resistance for helm stations, salon banquettes, and executive charter aircraft.
Key regulatory and consumer shifts defining commercial sourcing and contract fulfillment in Central America.
Panamanian luxury retailers are increasingly adopting European ESG guidelines, rejecting toxic chromium-tanned goods in favor of circular, biodegradable vegetable-tanned hides certified by the Leather Working Group.
Consignees in Panama City utilize bonded warehousing to break bulk shipments from India into just-in-time regional distribution batches across Central America, reducing localized inventory carrying expenses.
Panama's status as a multinational banking capital drives extensive corporate demand for executive refillable travel folios, RFID-shielded cardholders, and bespoke leather desk accessories with subtle blind debossing.
Terminal de Cruceros de Amador and Colon 2000 passenger footfalls increasingly demand authentically crafted, sustainable artisanal leather handbags that tell an authentic craft story without contributing to plastic waste.
Clear, unvarnished commercial, technical, and regulatory intelligence for sourcing directors, brand founders, and import procurement managers.
Every commercial invoice and bill of lading is supported by certified laboratory test reports (SGS / TÜV) validating compliance with European Standard EN 15987, confirming zero detectable Chromium VI, zero azo-dyes, lead safety, and formal REACH Annex XVII chemical adherence required for global and Panamanian trade.
We routinely ship CIF or FOB to both Puerto Balboa (Pacific) and Puerto Manzanillo / Colon (Atlantic). Our export documentation package includes legalized Commercial Invoices, Packing Lists, Certificates of Origin, and Phytosanitary / Tannery Declaration Certificates required by the National Customs Authority of Panama (Autoridad Nacional de Aduanas).
Yes. By consigning the shipping documents directly to your licensed forwarder or registered commercial warehouse within the Zona Libre de Colón (ZLC), goods enter under the suspended tax regime, permitting re-export across Latin America without incurring local Panamanian import duties or 7% ITBMS taxes.
For custom manufactured bags and leather folios, our typical entry MOQ is 100 to 200 units per style/colorway, supported by fast-track proto sampling within 10 to 14 business days. For bulk upholstery rolls and cut hides, MOQ starts at 1,000 square feet per custom color specification.
We deploy food-grade, micro-encapsulated anti-mold chips (such as Micro-Pak) within individual breathable dust bags, double-seal master export cartons with moisture barriers, and install heavy-duty container desiccants to completely eliminate "container rain" during trans-pacific maritime carriage.
Yes. We integrate high-attenuation Faraday-grade metallic shielding cloth beneath the grain leather lining of all travel wallets and card cases, providing complete multi-band RFID blocking (13.56 MHz to 860-960 MHz) to protect corporate and international travelers.
Combining second-generation industrial precision with certified ethical compliance and globally audited tanneries.
As a female-founded and female-led industrial business founded in 1996, our workshops operate under Sedex SMETA 4-Pillar audits, ensuring fair living wages, rigorous health and safety protocols, and zero environmental exploitation in our Kolkata facilities.
Every square foot of vegetable-tanned cowhide, calfskin, and buff leather is sourced strictly from Leather Working Group (LWG) certified tanneries implementing closed-loop effluent treatment plants (ETP) and renewable water recovery systems.
We work directly from your 2D design briefs, technical sketch packs, or physical reference samples. Our sample room builds precision paper patterns, selects custom pantone-matched hides, and provides physical master counter-samples in less than two weeks.
Initiate a direct production consultation with our senior technical merchandising team. Review certified material swatches, examine test documentation, and obtain firm volume quotations for delivery into Panama City or the Colon Free Zone.